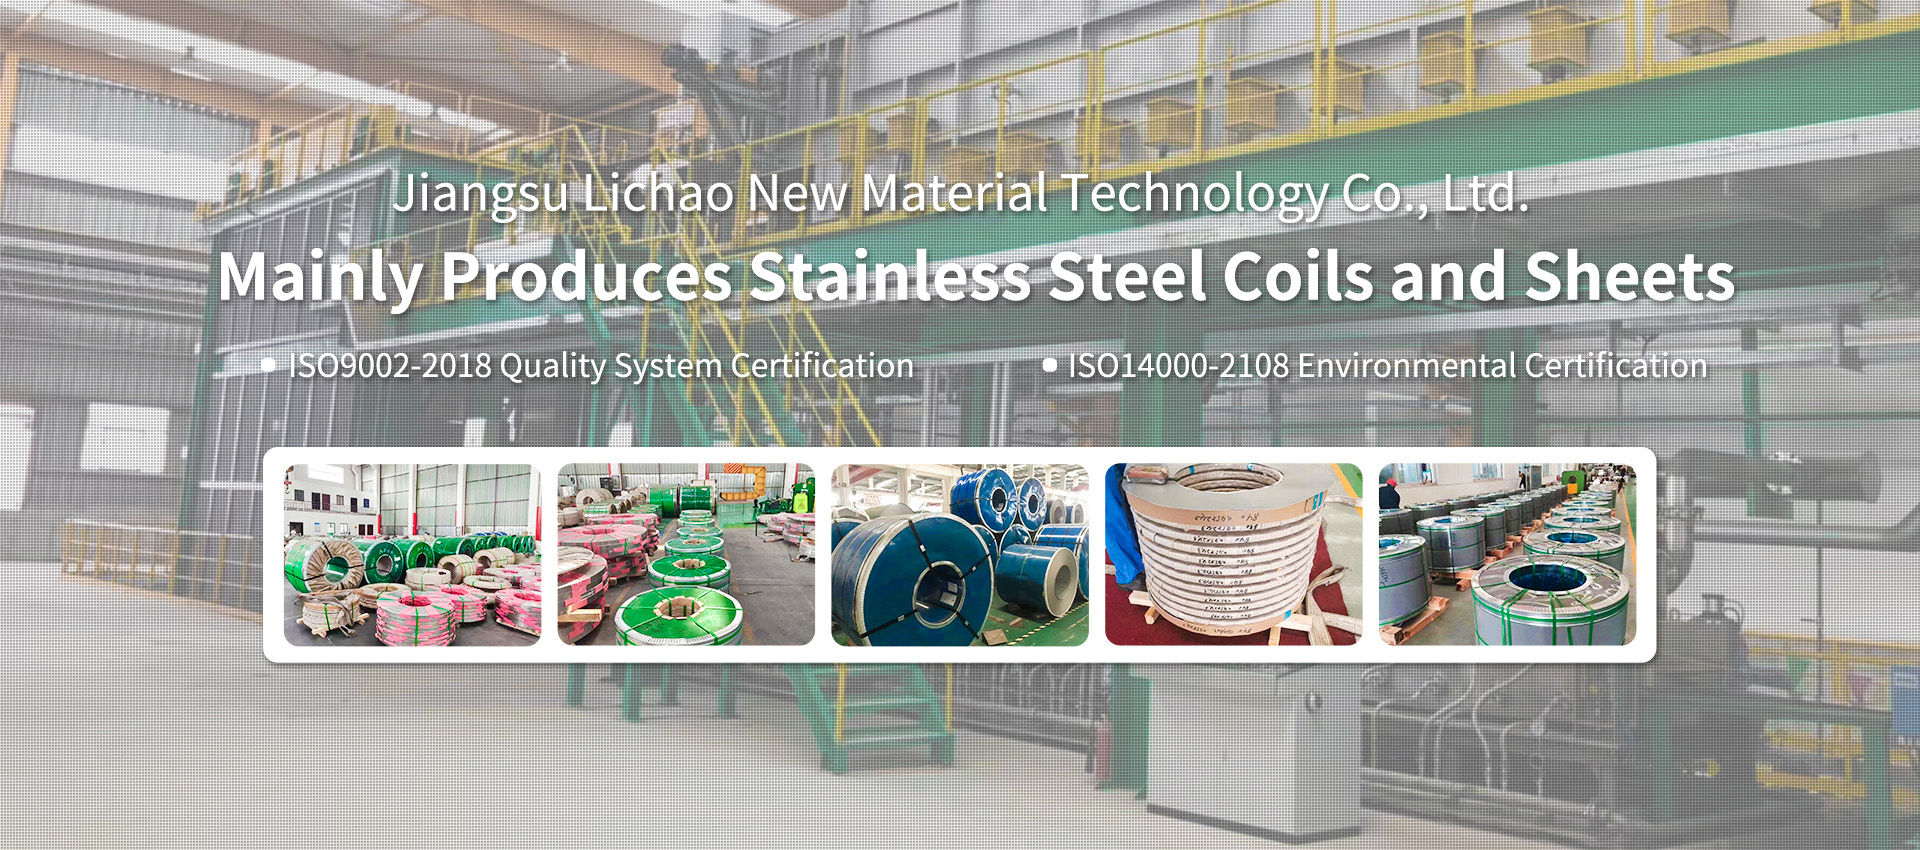
Welcome to Jiangsu Lichao New Material Technology Co., Ltd.




Intimate service comes from the recognition of customers, and proposes high-quality product matching solutions according to customer needs
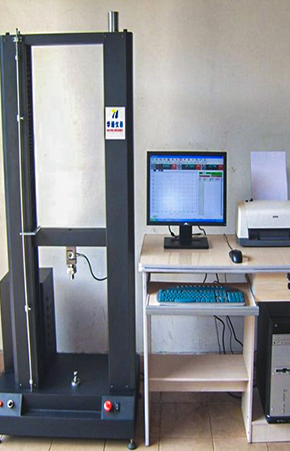
Product quality comes from rigorous and perfect quality control, and every step is full of our strict sense of responsibility
Exclusive customization comes from personalized configuration solutions, timely and efficient supporting new product development and production
Fast distribution originates from sufficient inventory + processing + fast logistics, and upholds enthusiastic and efficient management
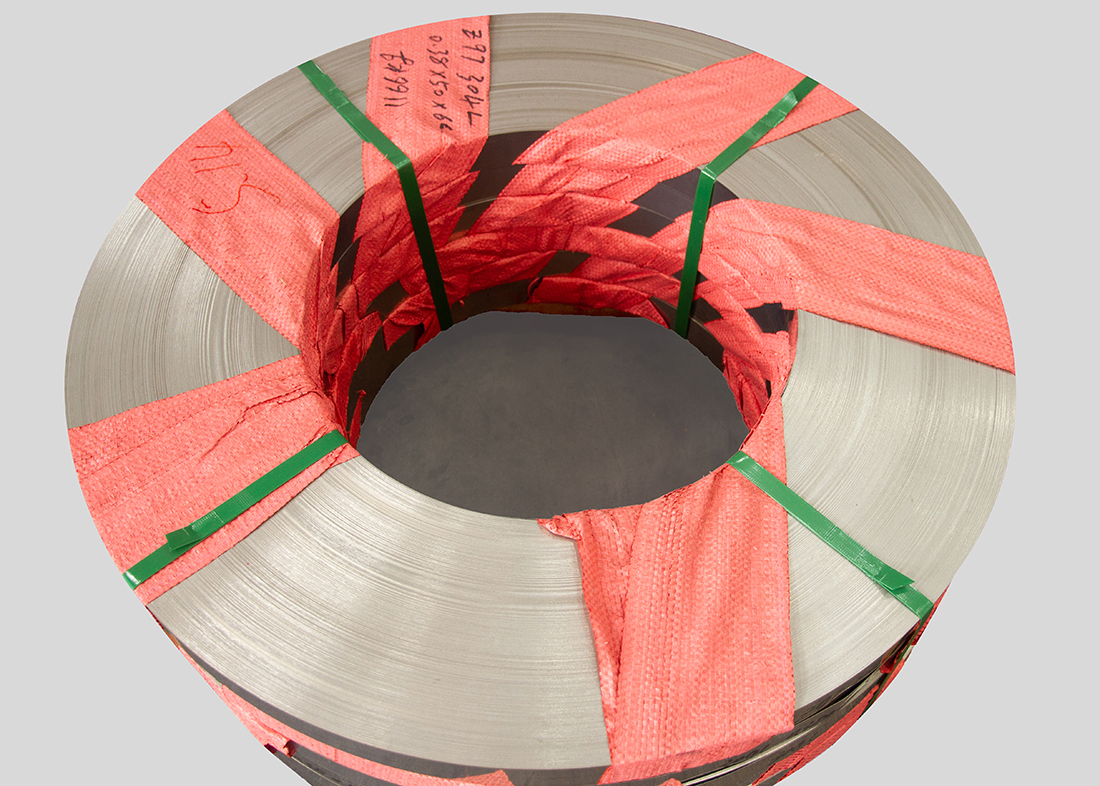
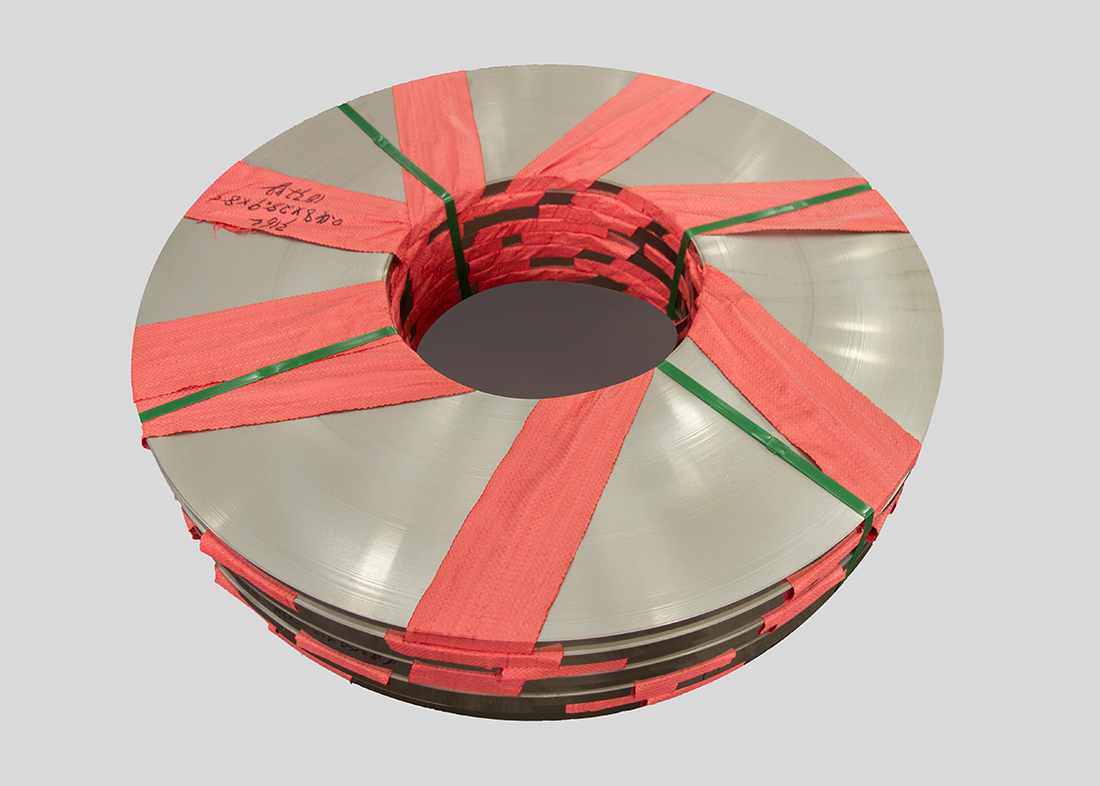
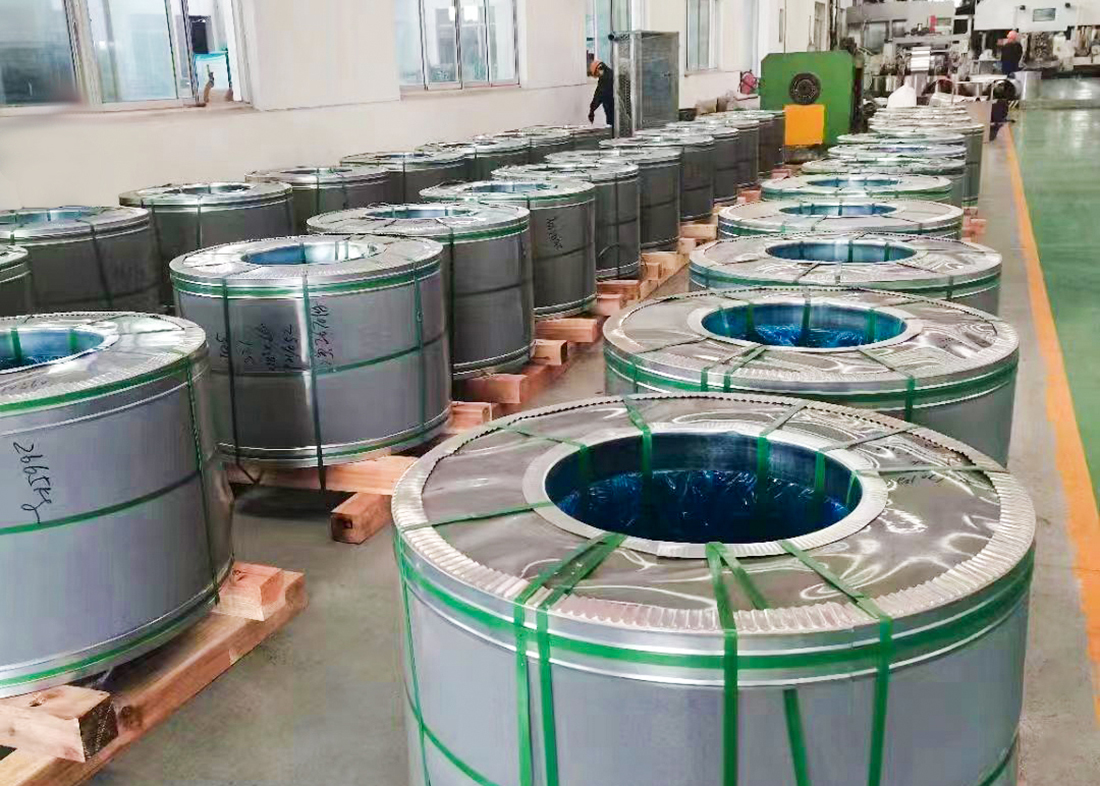
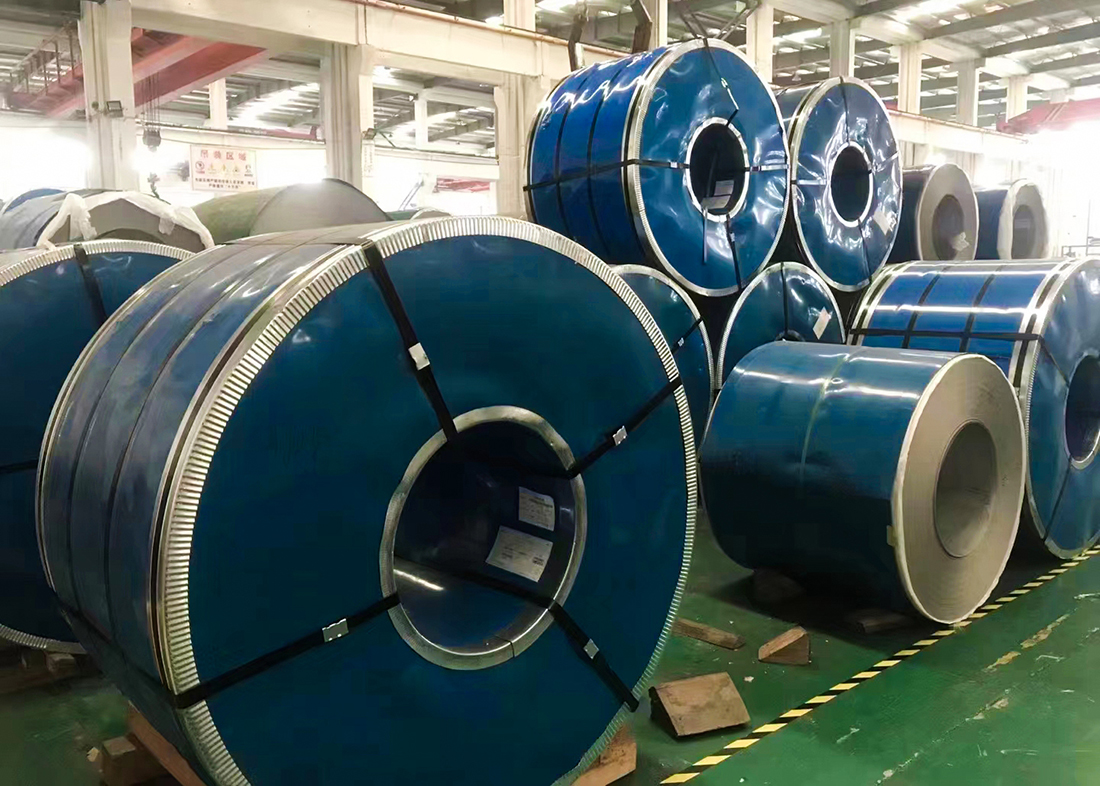
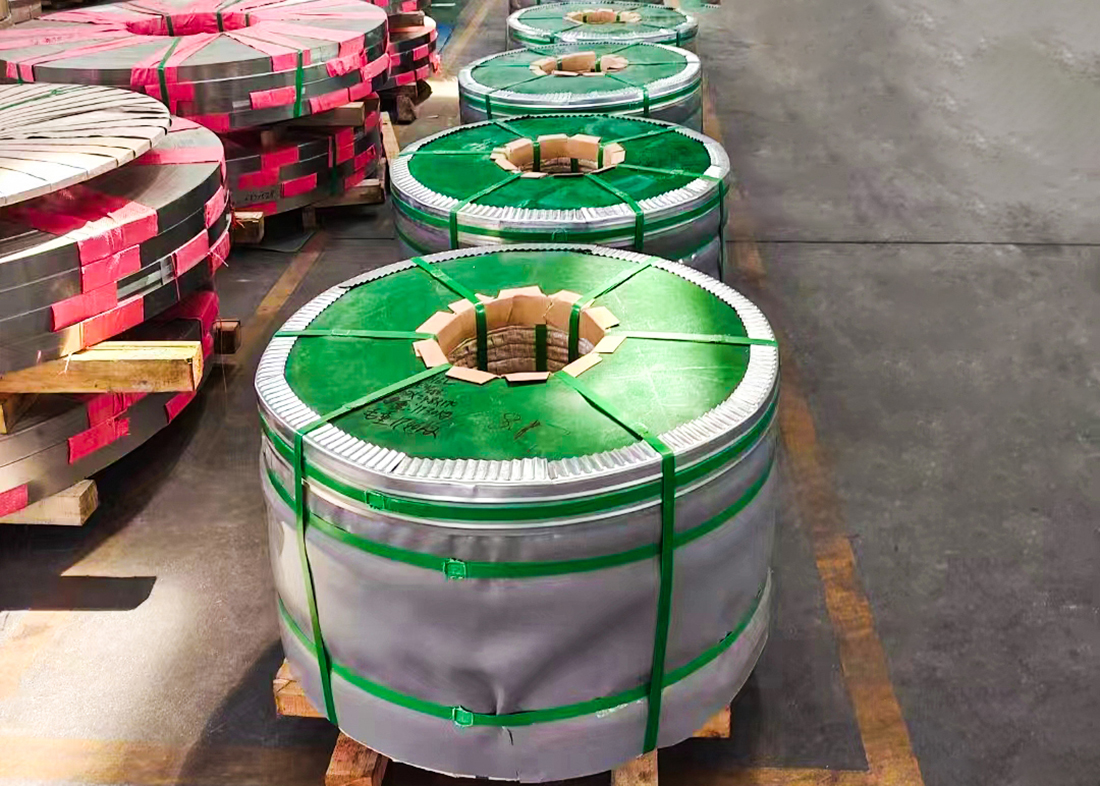

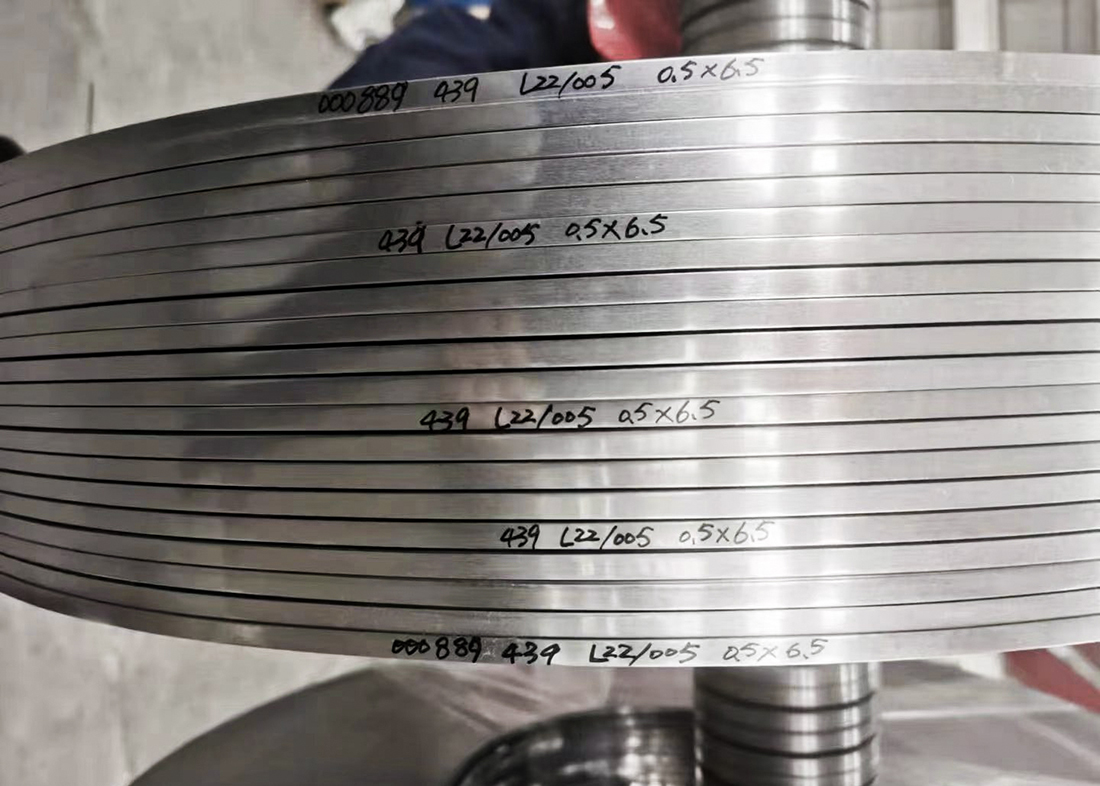
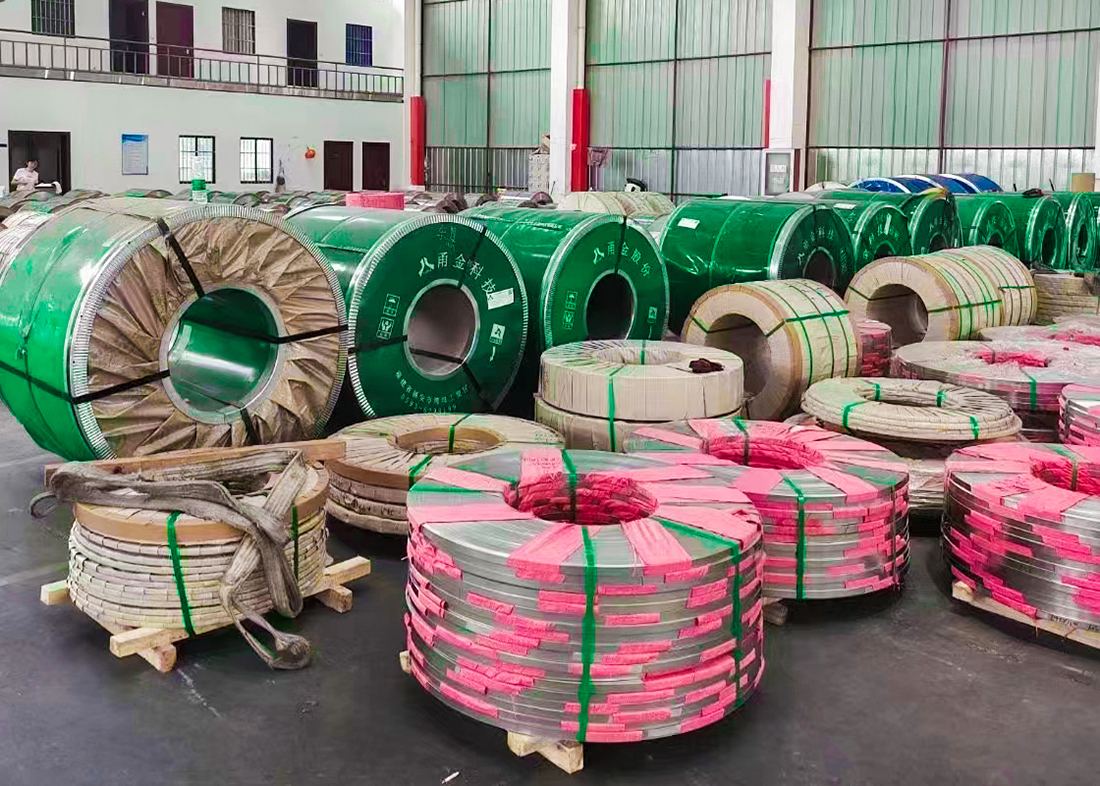
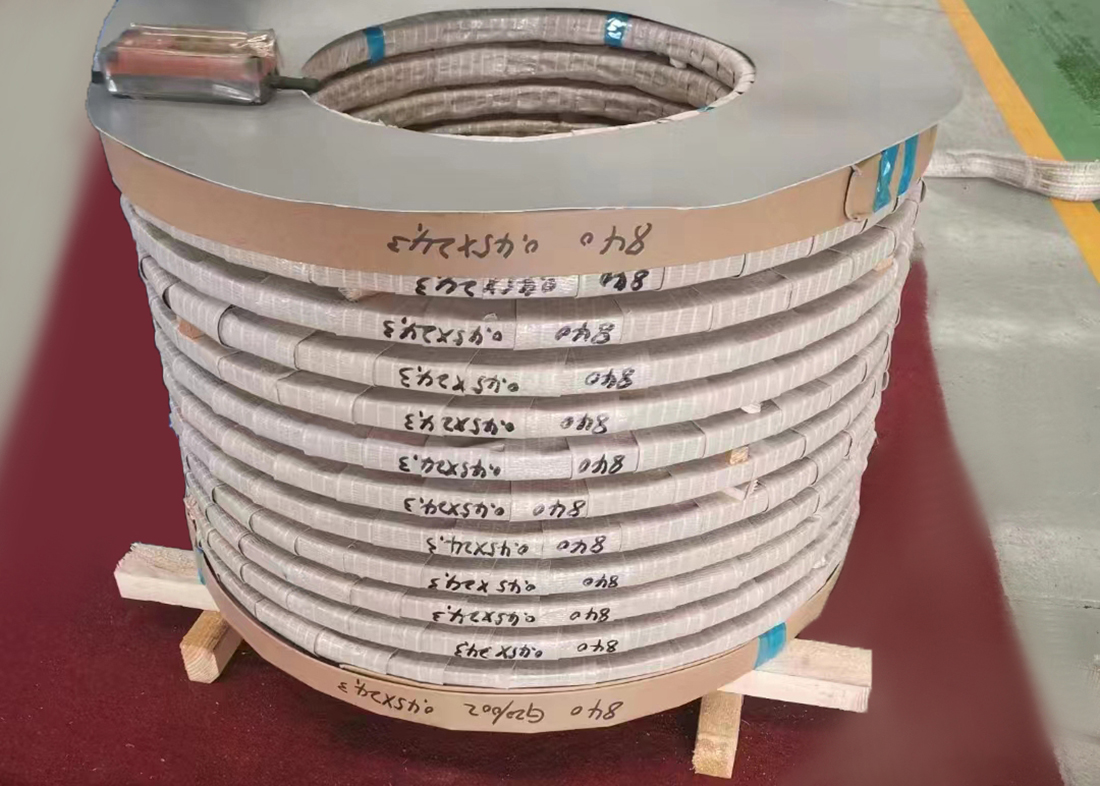





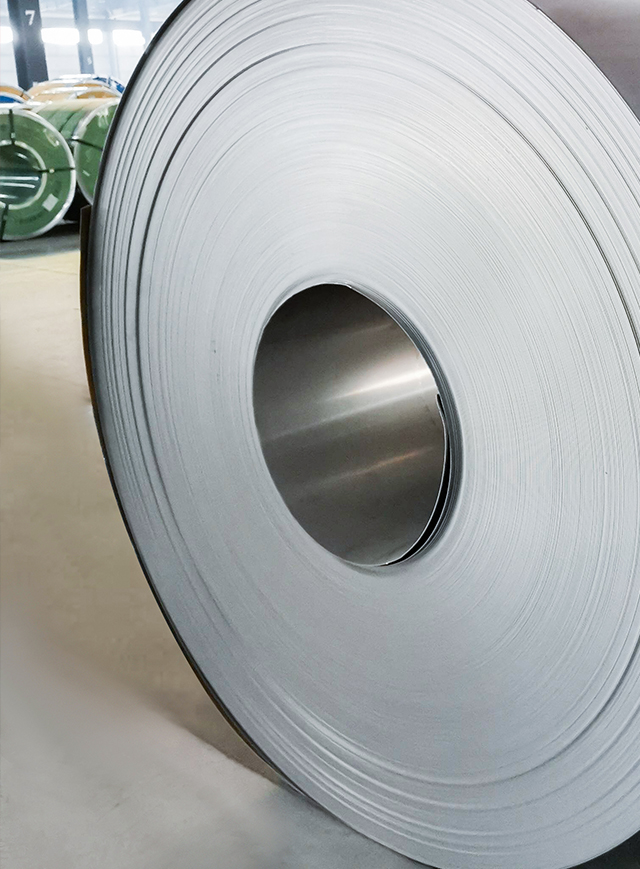
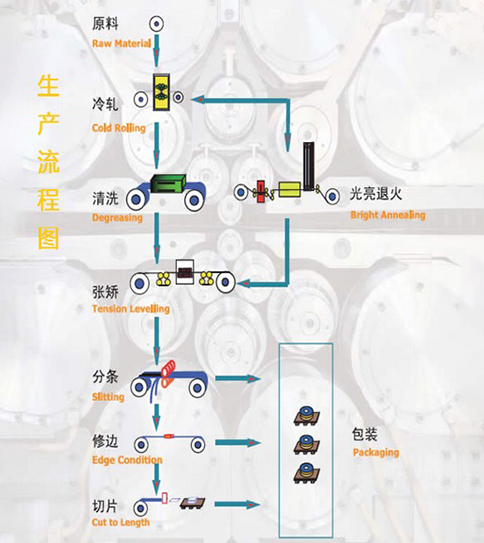
From raw material detection to warehousing registration management, to ensure the overall quality of products
From surface treatment to standard comparison
From material cutting and processing control to re-inspection, packaging and delivery
Every step is full of our strict sense of responsibility

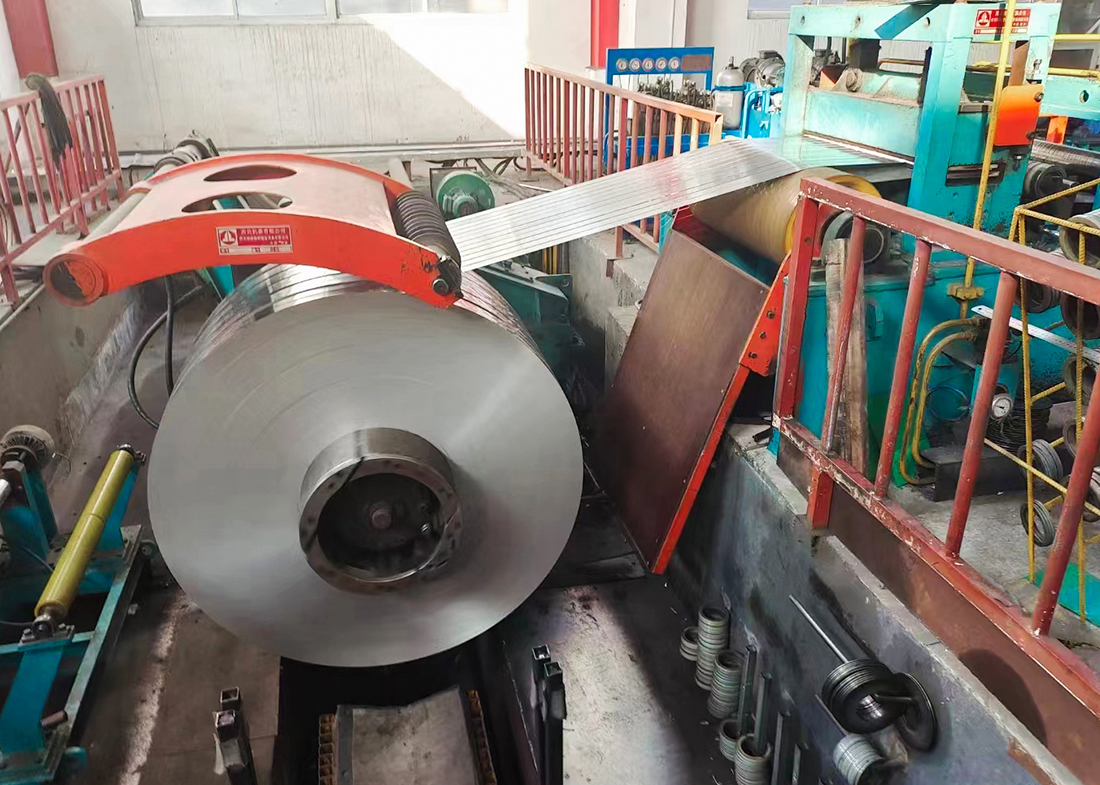
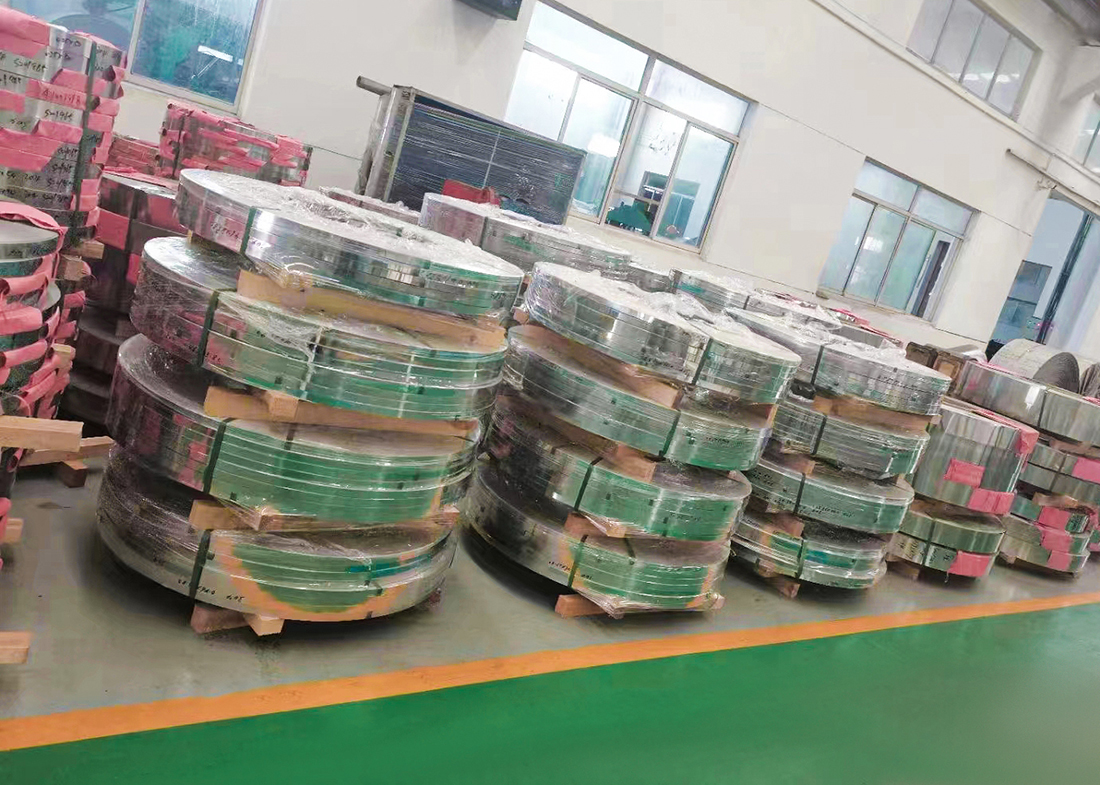
Special material stainless steel is mainly produced with a thickness of 0.02mm-3.1mm and a width of 1mm-1500mm
Relying on the company's domestic and foreign processing equipment and logistics network throughout the country
From customer orders to fit stock screening
Then to processing, production, re-inspection and distribution
Our R&D team has established good cooperative relations with domestic and foreign steel mills
Timely and efficient cooperation with customers for product development
Combined with a Japanese-funded continuous electroplating factory, we have successfully launched gold-plated, silver-plated, nickel-plated and other electroplating products.
Products have broad market prospects and development potential

Stainless steel materials have high deformation resistance and obvious work hardening. Thin gauge strips are prone to defects such as medium waves, edge waves, quarter waves, and single-sided waves. Generally, roller system mechanical adjustment, segmented cooling, tension control, roller profile pre configuration, online plate shape closed-loop detection, and subsequent leveling and straightening
1. Nitric acid immersion passivation (traditional chemical passivation) Soak the stainless steel strip in nitric acid bath to remove surface free iron impurities and promote chromium oxidation to form a dense passivation film. Can be divided into multiple concentration levels, suitable for austenitic stainless steels such as 304 and 316; The disadvantage is the generation of nitrogen oxide
Stainless steel relies on the passivation film of chromium on the surface to prevent corrosion; Chloride ions can penetrate the passivation film, preventing widespread uniform rusting and making it more prone to pitting and crevice corrosion. Under high temperature and tensile stress conditions, austenitic steel may also experience stress corrosion cracking.
Stainless steel strip protective film (mainly PE protective film) is used to protect the surface of the board during storage, cutting, bending, and stamping processes, preventing scratches, indentations, and dust pollution. The selection of the film coating needs to match the surface type, processing technology, service environment, and peeling time of the stainless steel, referring to GB/T 20878
Flattening, also known as smoothing, is a small reduction rate rolling process after cold rolling and annealing. The reduction rate is usually only 0.5-3%, without changing the material thickness specifications. It relies on the rolling mill to lightly press the surface of the steel strip, and its main functions are as follows:
1、 At the material level (source priority) 1. Reasonably reduce the hardness of materials For the same grade, the lower the hardness, the higher the elongation, and the smaller the rebound. Example: The original rebound of 301-3/4H was too large. If conditions permit, it can be changed to 301-1/2H, and the rebound will significantly decrease; The cost is a decrease in elasticity, an

Stainless steel coils are widely used in various equipment manufacturing, pipeline systems, container lining and other scenarios in the chemical industry due to their excellent corrosion resistance, high temperature resistance, strength and processability. They are the core material for dealing with complex media (such as acids, alkalis, salts, organic solvents, etc.) and harsh working conditions
1. Different production processes Stainless steel hot rolling is rolled above the recrystallization temperature of the metal material, and stainless steel cold rolling is rolled below the recrystallization temperature of the metal material, and each metal material has its own recrystallization temperature. crystallization temperature.
Stainless steel materials have high deformation resistance and obvious work hardening. Thin gauge strips are prone to defects such as medium waves, edge waves, quarter waves, and single-sided waves. Generally, roller system mechanical adjustment, segmented cooling, tension control, roller profile pre configuration, online plate shape closed-loop detection, and subsequent leveling and straightening
1. Nitric acid immersion passivation (traditional chemical passivation) Soak the stainless steel strip in nitric acid bath to remove surface free iron impurities and promote chromium oxidation to form a dense passivation film. Can be divided into multiple concentration levels, suitable for austenitic stainless steels such as 304 and 316; The disadvantage is the generation of nitrogen oxide
Stainless steel relies on the passivation film of chromium on the surface to prevent corrosion; Chloride ions can penetrate the passivation film, preventing widespread uniform rusting and making it more prone to pitting and crevice corrosion. Under high temperature and tensile stress conditions, austenitic steel may also experience stress corrosion cracking.
Stainless steel strip protective film (mainly PE protective film) is used to protect the surface of the board during storage, cutting, bending, and stamping processes, preventing scratches, indentations, and dust pollution. The selection of the film coating needs to match the surface type, processing technology, service environment, and peeling time of the stainless steel, referring to GB/T 20878
Flattening, also known as smoothing, is a small reduction rate rolling process after cold rolling and annealing. The reduction rate is usually only 0.5-3%, without changing the material thickness specifications. It relies on the rolling mill to lightly press the surface of the steel strip, and its main functions are as follows:
1、 At the material level (source priority) 1. Reasonably reduce the hardness of materials For the same grade, the lower the hardness, the higher the elongation, and the smaller the rebound. Example: The original rebound of 301-3/4H was too large. If conditions permit, it can be changed to 301-1/2H, and the rebound will significantly decrease; The cost is a decrease in elasticity, an
 Jiangsu Lichao New Material Technology Co., Ltd.
 WeChat ID:jinjiayi0512
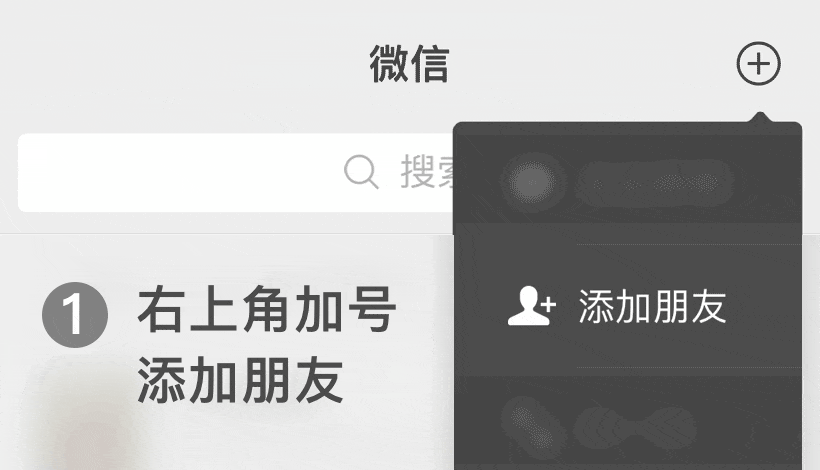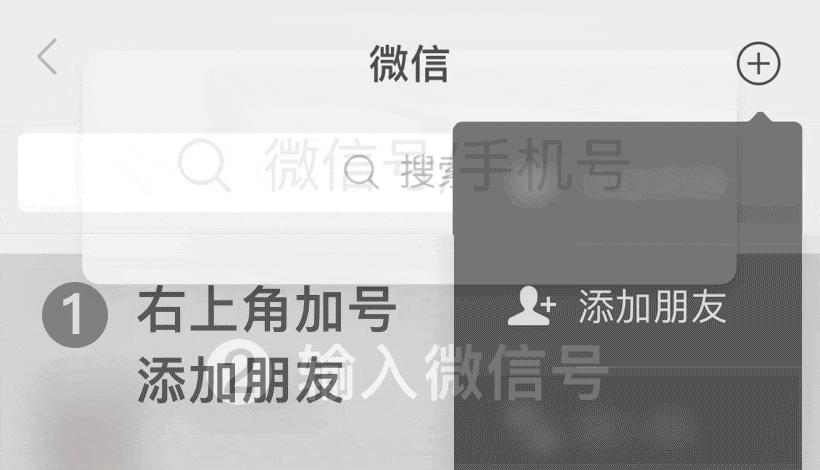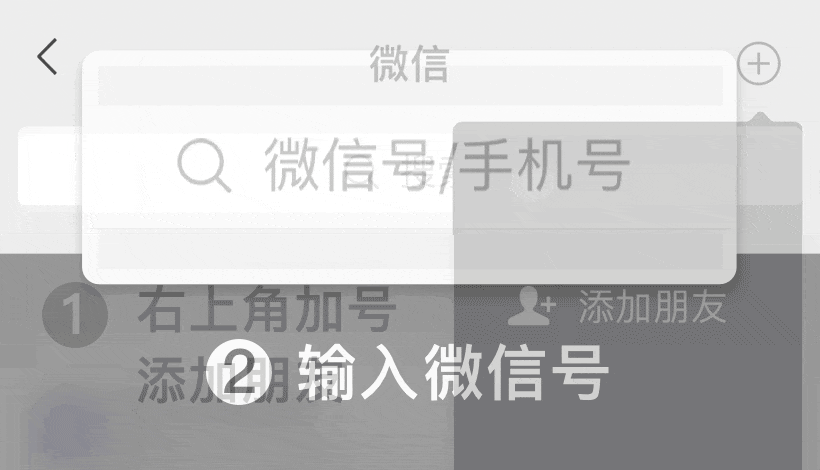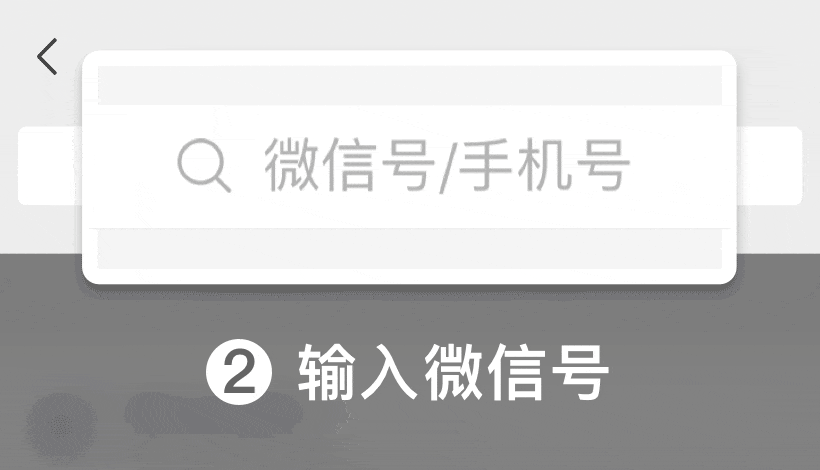


 Add WeChat
 Contact us
 The phone